Non classé
BMW’s Job Cuts Reveal the Real Battle Over Europe’s Automotive Supply Chain

Published
4 mois agoon
By
BMW has spent the past several years looking like the most composed member of Germany’s increasingly unsettled automotive industry.
Volkswagen has been trying to shrink a cost structure built for a larger European market. Porsche has struggled with falling demand in China. Mercedes-Benz has been cutting costs and reconsidering the breadth of its vehicle portfolio.
BMW appeared to have given itself more room to maneuver.
It continued investing in electric vehicles without committing its entire future to a single propulsion technology. Its factories retained the flexibility to build combustion, plug-in hybrid, and electric models. Its premium positioning also offered some protection from the price competition consuming the lower end of the market.
That strategy has not failed. But it has not insulated BMW from the forces now reshaping the European automotive industry.
BMW said in late July that it would eliminate several thousand positions in Germany by the end of 2027 through a voluntary severance program. The cuts are aimed at administrative and development functions, not production workers. Reuters, citing a person familiar with the plan, reported that BMW’s global workforce could eventually decline by roughly 8,000 positions. BMW has not publicly confirmed that figure.
The distinction matters.
This is not simply another automaker cutting factory employment because demand weakened. BMW is taking a harder look at how the company is managed, how decisions move through the organization, and how much overhead is required to develop and sell a vehicle.
At nearly the same time, France, Germany, and the European Commission are moving toward a more deliberate effort to keep automotive production and component value inside Europe.
The two developments belong together.
BMW is trying to become leaner and faster. Europe is preparing to make automotive sourcing more regional, more traceable, and more closely tied to public policy.
The first effort may simplify BMW. The second could make its supply chain considerably more complicated.
BMW’s Margins Leave Little Room for Delay
BMW’s second-quarter results explain why management is prepared to revisit structures that once appeared permanent.
Group profit before tax fell 35.1% from the previous year to €1.697 billion. Revenue declined 7.9% to €31.259 billion. Within the automotive segment, earnings before interest and taxes fell 60.7% to €629 million. The automotive operating margin dropped from 5.4% to 2.3%.
BMW attributed the pressure to lower volumes, intense competition in China, currency movements, higher depreciation, commodity costs, and additional U.S. tariffs. Tariffs alone reduced the automotive margin by approximately 1.25 percentage points during the second quarter and first half.
The company has already been cutting spending. Selling and administrative expenses in the automotive business fell 8.3% during the quarter. But those reductions were not enough to offset the deterioration in the market.
China remains the most immediate problem.
BMW Group deliveries in China fell 30.2% during the second quarter, from 168,959 vehicles to 117,927. Deliveries were down 20.4% for the first half. Global second-quarter deliveries declined 4.9%, despite growth in Europe and the United States.
China once provided German premium automakers with a powerful source of volume, profit, and confidence. Those earnings helped finance large engineering organizations, broad vehicle portfolios, and the enormous cost of developing the next generation of vehicles.
That economic engine is becoming less dependable.
Chinese automakers are no longer simply lower-cost competitors. They are developing new vehicles quickly, integrating software effectively, and competing most aggressively in the electric-vehicle segments where much of the industry’s investment is now concentrated.
BMW has reduced its expected 2026 automotive margin from 4%–6% to 1%–3%. It now expects deliveries to decline slightly and group profit before tax to fall significantly from the previous year.
Those numbers turn the discussion from incremental improvement to structural change.
The Next Restructuring Will Reach the Office
BMW’s decision to focus voluntary departures on administration and development says a great deal about where management believes the company has become too heavy.
Automotive complexity accumulated over decades. New regions, brands, technologies, regulations, and vehicle programs created new processes. Those processes created committees, specialists, interfaces, and layers of management.
That structure was easier to support when margins were higher and China was growing. It becomes much harder to justify when an automaker must simultaneously fund combustion engines, plug-in hybrids, battery-electric vehicles, software platforms, batteries, and autonomous-driving systems.
BMW’s new CEO, Milan Nedeljkovic, has said the company will revisit processes and structures that were previously considered untouchable. The review will extend across sales, procurement, production, and development. BMW also plans to reduce some model variants where demand no longer justifies the complexity.
That may matter more than the final number of job cuts.
A company can remove thousands of positions and still leave the underlying work untouched. The remaining employees simply inherit the same reports, approvals, meetings, and handoffs.
BMW’s real challenge is to remove work from the system.
That may mean fewer model combinations, fewer approval layers, tighter engineering priorities, and a more direct connection between product decisions and supplier execution.
Artificial intelligence will have a role in document-heavy areas such as procurement, engineering support, finance, and compliance. But the technology is not the central story.
The real test is whether BMW uses it to eliminate steps and shorten decision cycles, or merely asks a smaller workforce to operate the same complicated organization.
Germany’s Supplier Base Faces the Harder Transition
BMW’s restructuring will attract attention because of the company’s size. The more severe adjustment may occur among suppliers.
The German Association of the Automotive Industry estimates that the country lost roughly 100,000 automotive jobs between 2019 and 2025. It projects that another 125,000 could disappear by 2035 under current conditions.
Suppliers are caught between two technology systems.
They must continue supporting combustion vehicles that still generate substantial volume and cash flow. At the same time, they must invest in electric drivetrains, battery systems, power electronics, sensors, software, and thermal management.
The old business is expected to decline. The new business often lacks the scale or margins to replace it.
Automakers also continue pushing suppliers for cost reductions while those suppliers face higher European energy, labor, financing, and regulatory costs.
This is why European suppliers are pressing for a meaningful definition of “Made in Europe.”
Their concern is not simply where final assembly occurs. A vehicle can be assembled in Europe while much of its battery, electronics, materials, software, and component value comes from elsewhere.
Europe retains the assembly jobs but gradually loses the industrial capabilities that determine where engineering expertise, intellectual property, and future investment reside.
“Made in Europe” Becomes a Supply-Chain Rule
The European Commission’s proposed Industrial Accelerator Act is an attempt to reverse that drift.
Introduced in March, the proposal would increase demand for European-made, low-carbon industrial products and strengthen capacity in strategic sectors. For the automotive industry, it would connect selected public support and procurement programs to European assembly, regional content, and critical-component requirements.
The proposal has not yet completed the EU legislative process.
According to the framework described by the European automotive supplier association CLEPA, a qualifying vehicle would need to be assembled in the EU and meet a 70% regional-content threshold. A separate 50% threshold for designated critical components would take effect three years after the final regulation is published.
The political logic is straightforward. Europe does not want public money intended to support European industry flowing primarily into imported batteries, electronics, and other technologies.
The supply-chain implications are much less simple.
A 70% threshold turns the nationality of a vehicle into a data problem.
Automakers will need to know not only where final assembly occurred, but where the value inside the vehicle originated. That may require tracing battery cells, power electronics, semiconductors, magnets, software, castings, and raw-material processing across multiple supplier tiers.
Most automakers have strong visibility into tier-one suppliers. Visibility further upstream is far less consistent.
A battery pack may be assembled in Europe using cells produced elsewhere, materials processed in another country, and electronic controls from a third. A semiconductor may be designed in Europe, fabricated in Asia, and packaged in another region.
Regional-content rules will turn those relationships into eligibility decisions.
Procurement teams will have to consider whether a sourcing choice moves a vehicle above or below the threshold and whether that affects access to public incentives or government purchasing programs.
The least expensive component may no longer produce the lowest total cost.
Europe Can Buy Time, Not Competitiveness
There is a legitimate case for protecting critical European industrial capabilities.
China has used coordinated investment, financing, infrastructure, procurement, and industrial policy to build strong positions in batteries, electric vehicles, critical-material processing, and solar technology. The United States has also become more willing to connect public incentives to domestic production.
Europe is responding to a world in which its competitors are already managing industrial outcomes.
But regional-content rules cannot solve BMW’s core operating problems.
They cannot shorten vehicle-development programs, improve software, eliminate unnecessary approvals, restore Chinese demand, or guarantee that a European supplier is globally competitive.
Industrial policy may create time, demand, and investment incentives. BMW still has to use that time well.
That is the tension at the center of the story.
Europe is trying to preserve the automotive supply chain from the outside. BMW is trying to rebuild its competitiveness from the inside.
Both efforts may be necessary. Neither is sufficient on its own.
The future of Europe’s automotive industry will not be determined simply by how many vehicles are assembled in Munich, Stuttgart, Wolfsburg, or elsewhere in the EU.
The more important question is how much of the vehicle’s value is created there.
Europe could retain assembly plants while losing batteries, electronics, software, semiconductors, materials processing, and engineering. Cars would still leave European factories, but a smaller share of the economic and technological value would remain in Europe.
BMW’s cuts are therefore more than another automotive cost program. They are evidence that the next restructuring will extend through management, development, procurement, supplier networks, and the rules used to determine where a vehicle truly comes from.
Europe is preparing to defend its automotive industrial base.
BMW is preparing for the possibility that defense will only buy time.
The post BMW’s Job Cuts Reveal the Real Battle Over Europe’s Automotive Supply Chain appeared first on Logistics Viewpoints.
You may like
Non classé
When One Character Stops the Workflow: The Hidden Digital Dependencies of Modern Supply Chains
Published
4 heures agoon
22 novembre 2026By
A single misplaced character can stop a business process. I was reminded of that recently when a WordPress workflow supporting Logistics Viewpoints stopped functioning. After working through the failure, I found an unexpected double quotation mark at the end of the first line of a PHP file involved in the process. Removing it restored the workflow.
I had not deliberately edited the file, and I cannot establish how or when the character was introduced. A software update, hosting operation, automated process, inadvertent edit, or another cause is conceivable, but there is no evidence here to assign responsibility. Restoring the service solved the immediate problem. It did not establish its origin or guarantee that it could not happen again.
This was a small incident. Yet it exposed a dependence that is familiar to anyone running a modern supply chain: an otherwise useful system can become unavailable because one supporting component fails. The failure may occur far from the process that ultimately stops. For executives, the question is less whether individual applications are online than whether the business can still complete the work it depends on them to perform.
A Week That Exposed the Dependencies
November 2026 offered several much larger reminders. On November 12, Microsoft 365 experienced a major disruption affecting Exchange Online and other services. In its preliminary incident findings, Microsoft described a defect introduced in July that interacted with increased traffic and reduced gateway capacity. More than 80 percent of the affected gateway servers were unresponsive at the low point. A latent software issue became a major outage when operating conditions changed.
The logistics consequences were not theoretical. On November 13, Maersk advised customers that emails, notifications, and updates might be delayed and directed urgent inquiries to local office telephone numbers. A company’s TMS need not fail for its logistics operation to be impaired. If an essential communications channel is unavailable, a shipment exception may still go unresolved.
On November 13, the Federal Aviation Administration imposed a nationwide ground stop after a telecommunications failure destabilized services supporting air traffic control. The stop lasted approximately four hours and 45 minutes. The FAA’s account underscored the consequences of a failure in infrastructure connecting communications and radar information to real-world operations. Aircraft, crews, and cargo could not simply resume their original schedules the moment service returned.
On November 15, AWS reported signup, authentication, and connectivity problems in its US-East-1 region. The principal impact period was roughly three hours. These incidents were not connected, and their causes should not be conflated. Together, however, they show how communications, infrastructure, and supporting cloud services can become points of operational dependence even when a company’s primary business application remains functional.
When a Digital Failure Destroys Physical Inventory
An even more direct supply chain consequence appeared in European retail refrigeration. During October and November, attackers interfered with connected commercial refrigeration equipment in several countries. Stores discarded spoiled food after cooling systems were manipulated. Reuters reported on November 20 that British cybersecurity specialists had addressed a vulnerability following the attacks.
These were deliberate intrusions, not another example of a cloud outage or software defect. The distinction matters. The common management issue is that digital dependencies increasingly govern physical operating conditions. Connected refrigeration equipment, warehouse automation, material handling systems, and transport execution interfaces can turn a loss of software integrity or availability into damaged inventory, interrupted throughput, and missed customer commitments.
System Uptime Is Not Business Availability
Most technology organizations measure availability in familiar ways: server uptime, application response, incident duration, and contractual service levels. Those are important measures, but they do not necessarily tell a supply chain executive whether orders are moving and commitments are being fulfilled.
A WMS might remain accessible while the interface to an automated storage and retrieval system stops exchanging the messages needed to move inventory. A TMS can be operational while carrier communications or dock scheduling are unavailable. An AI-supported control tower can continue producing recommendations while a critical data feed has gone stale. In each instance, infrastructure metrics may look acceptable even as the business process is degraded.
This is why I would add business-process availability to the resilience discussion. Can orders move from release to confirmed fulfillment? Are shipment milestones being received within acceptable intervals? Are warehouse tasks completing, rather than merely being issued? Can a promised receiving appointment be verified in the scheduling record? These questions connect observability to actual execution.
The distinction has practical implications for technology sourcing and architecture. A vendor’s uptime commitment is not the same as a guarantee that an end-to-end order, transportation, or warehouse process will complete. Integration points, third-party services, exception handoffs, and the quality of underlying data must be treated as elements of operational performance, not simply as technical support issues.
Restoration Is Not Root-Cause Analysis
The PHP-file incident illustrates another important distinction. Removing the unexpected quotation mark restored an import process, but it did not explain why the file had changed. A successful workaround, rollback, or component restart demonstrates that the process can recover. It does not necessarily identify the initiating failure or establish that recurrence has been prevented.
Microsoft’s November outage presents the enterprise-scale version of that problem. The software defect had been present for months. The serious disruption emerged only when traffic and capacity conditions exposed it. Testing an individual component in isolation would not necessarily have revealed the risk created by that particular combination of conditions.
Resilience therefore requires more than rapid troubleshooting. It requires controlled changes, configuration integrity, useful logs, tested rollback paths, and validation that recovered systems are actually completing transactions. It also requires investigations grounded in evidence. An unexplained file change should not be labeled a cyberattack, a provider defect, or operator error without support.
Design Resilience Around the Work, Not Just the Software
For supply chain leaders, I see four practical priorities. First, map the technology dependencies of the business processes that most directly affect service, safety, inventory, and cash flow. That map should include communications services, identity systems, third-party integrations, cloud platforms, and operational technology, not just the ERP, WMS, or TMS at the center of the workflow.
Second, monitor transaction completion. An application being reachable is necessary but insufficient. Organizations need to detect when orders stop advancing, when shipment events go missing, when inventory tasks fail to reconcile, or when interfaces silently stop delivering useful data. The operational owner should receive an actionable alert before a hidden dependency becomes a customer failure.
Third, test controlled degradation. What happens if email is unavailable, an identity provider fails, an automated warehouse interface becomes unreliable, or real-time transportation data disappears? Some activities may continue through alternate channels or manual controls. Others should stop safely rather than proceed with questionable information. Recovery plans should specify decision rights as clearly as technical steps.
Finally, validate restoration at the process level. Reconnecting an integration is not the same as proving that queued transactions completed correctly. Reconciliation, exception review, and confirmation against systems of record are essential, particularly where automated execution or AI agents can initiate changes without continuous human supervision.
Supply chain executives routinely examine single-source suppliers, geographic concentrations, inventory buffers, and transportation bottlenecks. Digital concentration and dependency risk deserve the same discipline. More connected and intelligent systems can deliver real value, but each new integration can also create another way for operational work to stop. The next measure of supply chain resilience will be whether critical business processes remain dependable when individual technologies do not.
The post When One Character Stops the Workflow: The Hidden Digital Dependencies of Modern Supply Chains appeared first on Logistics Viewpoints.
Non classé
Always-On AI Is Coming to Supply Chains. But Who Owns the Exception?
Published
1 jour agoon
21 novembre 2026By
The supply chain industry has invested heavily in detecting problems sooner. Transportation visibility systems identify late shipments, planning applications flag shortages, and control towers consolidate operational alerts. Yet knowing about an exception and resolving it are two different things. The delay may be visible to everyone, while responsibility for the next action remains surprisingly unclear.
That gap is becoming more important as artificial intelligence moves beyond answering questions and begins maintaining responsibility for work over time. On November 19, OpenAI expanded access to ChatGPT Dots, its persistent agents, to eligible ChatGPT Business Standard users, while testing access with a limited group of Plus subscribers. The agents can retain useful context, work with authorized applications, and pursue continuing assignments. This is not the same as releasing an autonomous transportation management system. It does, however, point toward an operating model that supply chain leaders should be examining.
The critical question is not whether an AI agent can produce a better recommendation. It is whether an organization can assign a bounded operational responsibility, know who is accountable for the result, and verify that the work was actually completed.
The Supply Chain Has an Execution Gap
Consider how many logistics exceptions are managed today. A late container generates an alert. A transportation planner checks the revised estimated arrival, calls the carrier, and coordinates with a distribution center. Someone may approve a new receiving window or an inventory transfer. But the work does not end when the recommendation is accepted. The carrier must acknowledge the change, the appointment must be updated, and the revised plan must hold up as conditions change.
A great deal of operational effort is spent in the intervals between those actions. Employees chase confirmations, reconstruct previous conversations, and determine whether an apparent resolution was reflected in the system of record. Enterprise applications support the process, but they do not always maintain a single durable record of who owns the exception through closure.
Persistent AI could improve this situation by preserving the case history, recognizing when new information changes its significance, and continuing to monitor outstanding actions. The benefit is not simply an answer that arrives in seconds. It is potentially less time between identifying an exception, deciding what to do, and confirming that the decision produced the intended operational result.
A New Class of Agents, Not a New TMS
The foundation-model providers are approaching persistent work from different directions. OpenAI’s Dots emphasize ongoing assignments supported by connected applications and dedicated computing environments. Anthropic’s Claude Managed Agents provide infrastructure for long-running, bounded execution, including retained state, tool controls, and scheduled activity. Google’s Gemini enterprise initiatives emphasize organizational integration, permissions, and governance. xAI’s Grok Bot 1.0 emphasizes collaborative agents that can recognize unfinished team activities and follow up.
These are different products with different degrees of maturity and integration. Their common direction is more important than their marketing similarities: AI is progressing from episodic interaction toward sustained work. None should be assumed capable of managing production-critical logistics transactions without appropriate enterprise architecture, validated integrations, and operational controls.
That distinction matters. Scheduled research, monitoring an inbox, retrieving shipment status, changing an appointment, and committing a freight expenditure are not interchangeable capabilities. As autonomy increases, the required standard for identity, data quality, permissions, auditability, and error recovery increases with it.
Follow the Exception to Its Actual Conclusion
Imagine a retailer with an inbound shipment of promotional merchandise approaching a regional distribution center. A visibility system reports a delay. The TMS holds carrier and shipment information, the WMS manages receiving capacity, and the ERP and order systems establish inventory requirements and customer commitments. The immediate question is whether the revised arrival threatens service or creates avoidable cost.
An AI agent assigned to investigate could gather those inputs, compare alternatives, and prepare a recommended receiving or fulfillment plan. As the arrival estimate changes, it could retain what was previously considered, which assumptions remain valid, and which decisions are pending. That continuity avoids repeatedly starting the investigation from scratch.
But the more important test comes after a planner approves a different receiving appointment. Was the carrier notified? Did it accept the arrangement? Was the appointment changed in the authoritative scheduling system? Did the warehouse have the promised capacity? If a later delay invalidated the plan, did the exception reopen and reach the right person?
An agent that offers an excellent recommendation and then loses track of its execution has not closed the exception. It has shifted the remaining work to someone else. The opportunity for persistent AI is to keep that bounded responsibility visible until the required evidence of completion exists, while escalating decisions that exceed its authority.
Assign the Work Without Surrendering Accountability
In a recent Logistics Viewpoints discussion of who controls the supply chain’s AI decision layer, I examined the competition among model providers, enterprise application vendors, and orchestration platforms. Ownership of the decision architecture is one question. Ownership of the work following a decision is another. An enterprise can have powerful optimization capabilities and still struggle with incomplete handoffs.
This argues for a straightforward operating discipline. Every persistent exception should have an identified business owner, a responsible workflow or agent, a defined next action, a deadline or reassessment trigger, an escalation path, and explicit closure criteria. Those attributes should be held in durable case state, with references back to authoritative records. They cannot depend solely on a model’s conversational memory.
I would also separate three levels of authority. Observation permits an agent to retrieve data, compare conditions, and monitor progress. Recommendation permits it to propose a response for approval. Execution permits it to modify records or commit resources, and should require controls proportionate to the financial and operational consequences. A carrier appointment change, an inventory allocation, and a customer delivery promise may require different approval rules even when they originate from the same exception.
Protocols such as Model Context Protocol and agent-to-agent messaging can simplify access and coordination. They do not, by themselves, create a durable operational record, verify transactions, or resolve the question of business accountability. The architecture must still reconcile agent activity with what the TMS, WMS, ERP, and other systems of record actually show.
The Economic Test Is the Resolved Case
Executives should resist measuring persistent AI by the number of tasks performed, messages generated, or hours an agent appears to be active. An agent that repeatedly checks shipment status without changing an outcome can create additional cost while adding little value. The relevant economic unit is the satisfactorily resolved exception.
Consider an illustrative transportation organization handling 200 exceptions per week. If better investigation and follow-up release an average of 15 minutes of manual effort per case, that represents 50 gross staff hours weekly. It is a useful starting estimate, not a verified savings figure. Human review, failed attempts, integration expenses, model usage, and oversight must be included before calculating net return.
More consequential gains may come from avoiding an expedited shipment, reducing detention, preventing a production interruption, or protecting a customer commitment. A credible pilot should therefore measure time to assessment, time awaiting approval, time to verified completion, reopened cases, intervention rates, and the total cost per resolved exception. These measures distinguish productive persistence from continuous activity.
Start with Work That Repeatedly Stalls
The best initial candidates are information-intensive processes requiring repeated follow-up but limited transaction authority: delayed inbound loads, supplier confirmations, purchase order discrepancies, inventory shortages, and customer order escalations. Select one exception category, establish its closure criteria, and compare agent-supported handling with the current process across the full life of each case.
The evaluation should include changed arrival times, missing data, unavailable integrations, competing priorities, and handoffs between employees. It should also establish when the agent must stop, ask for approval, or return control to a human operator. Successful demonstrations are less important than dependable behavior when the process becomes messy.
AI’s progression toward always-on work is significant, but it should not be confused with a near-term transition to fully autonomous supply chains. The harder problem remains coordinating people, processes, technology, and decision rights across the enterprise. The most valuable agent may not be the one that first identifies a late shipment. It may be the one that helps the organization establish, with evidence, that the problem was actually resolved.
The post Always-On AI Is Coming to Supply Chains. But Who Owns the Exception? appeared first on Logistics Viewpoints.
Non classé
Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy
Published
2 jours agoon
20 novembre 2026By
An analyst perspective on why orchestration, digital twins, and plant-floor integration matter more than the robot alone
Production logistics becomes a control problem
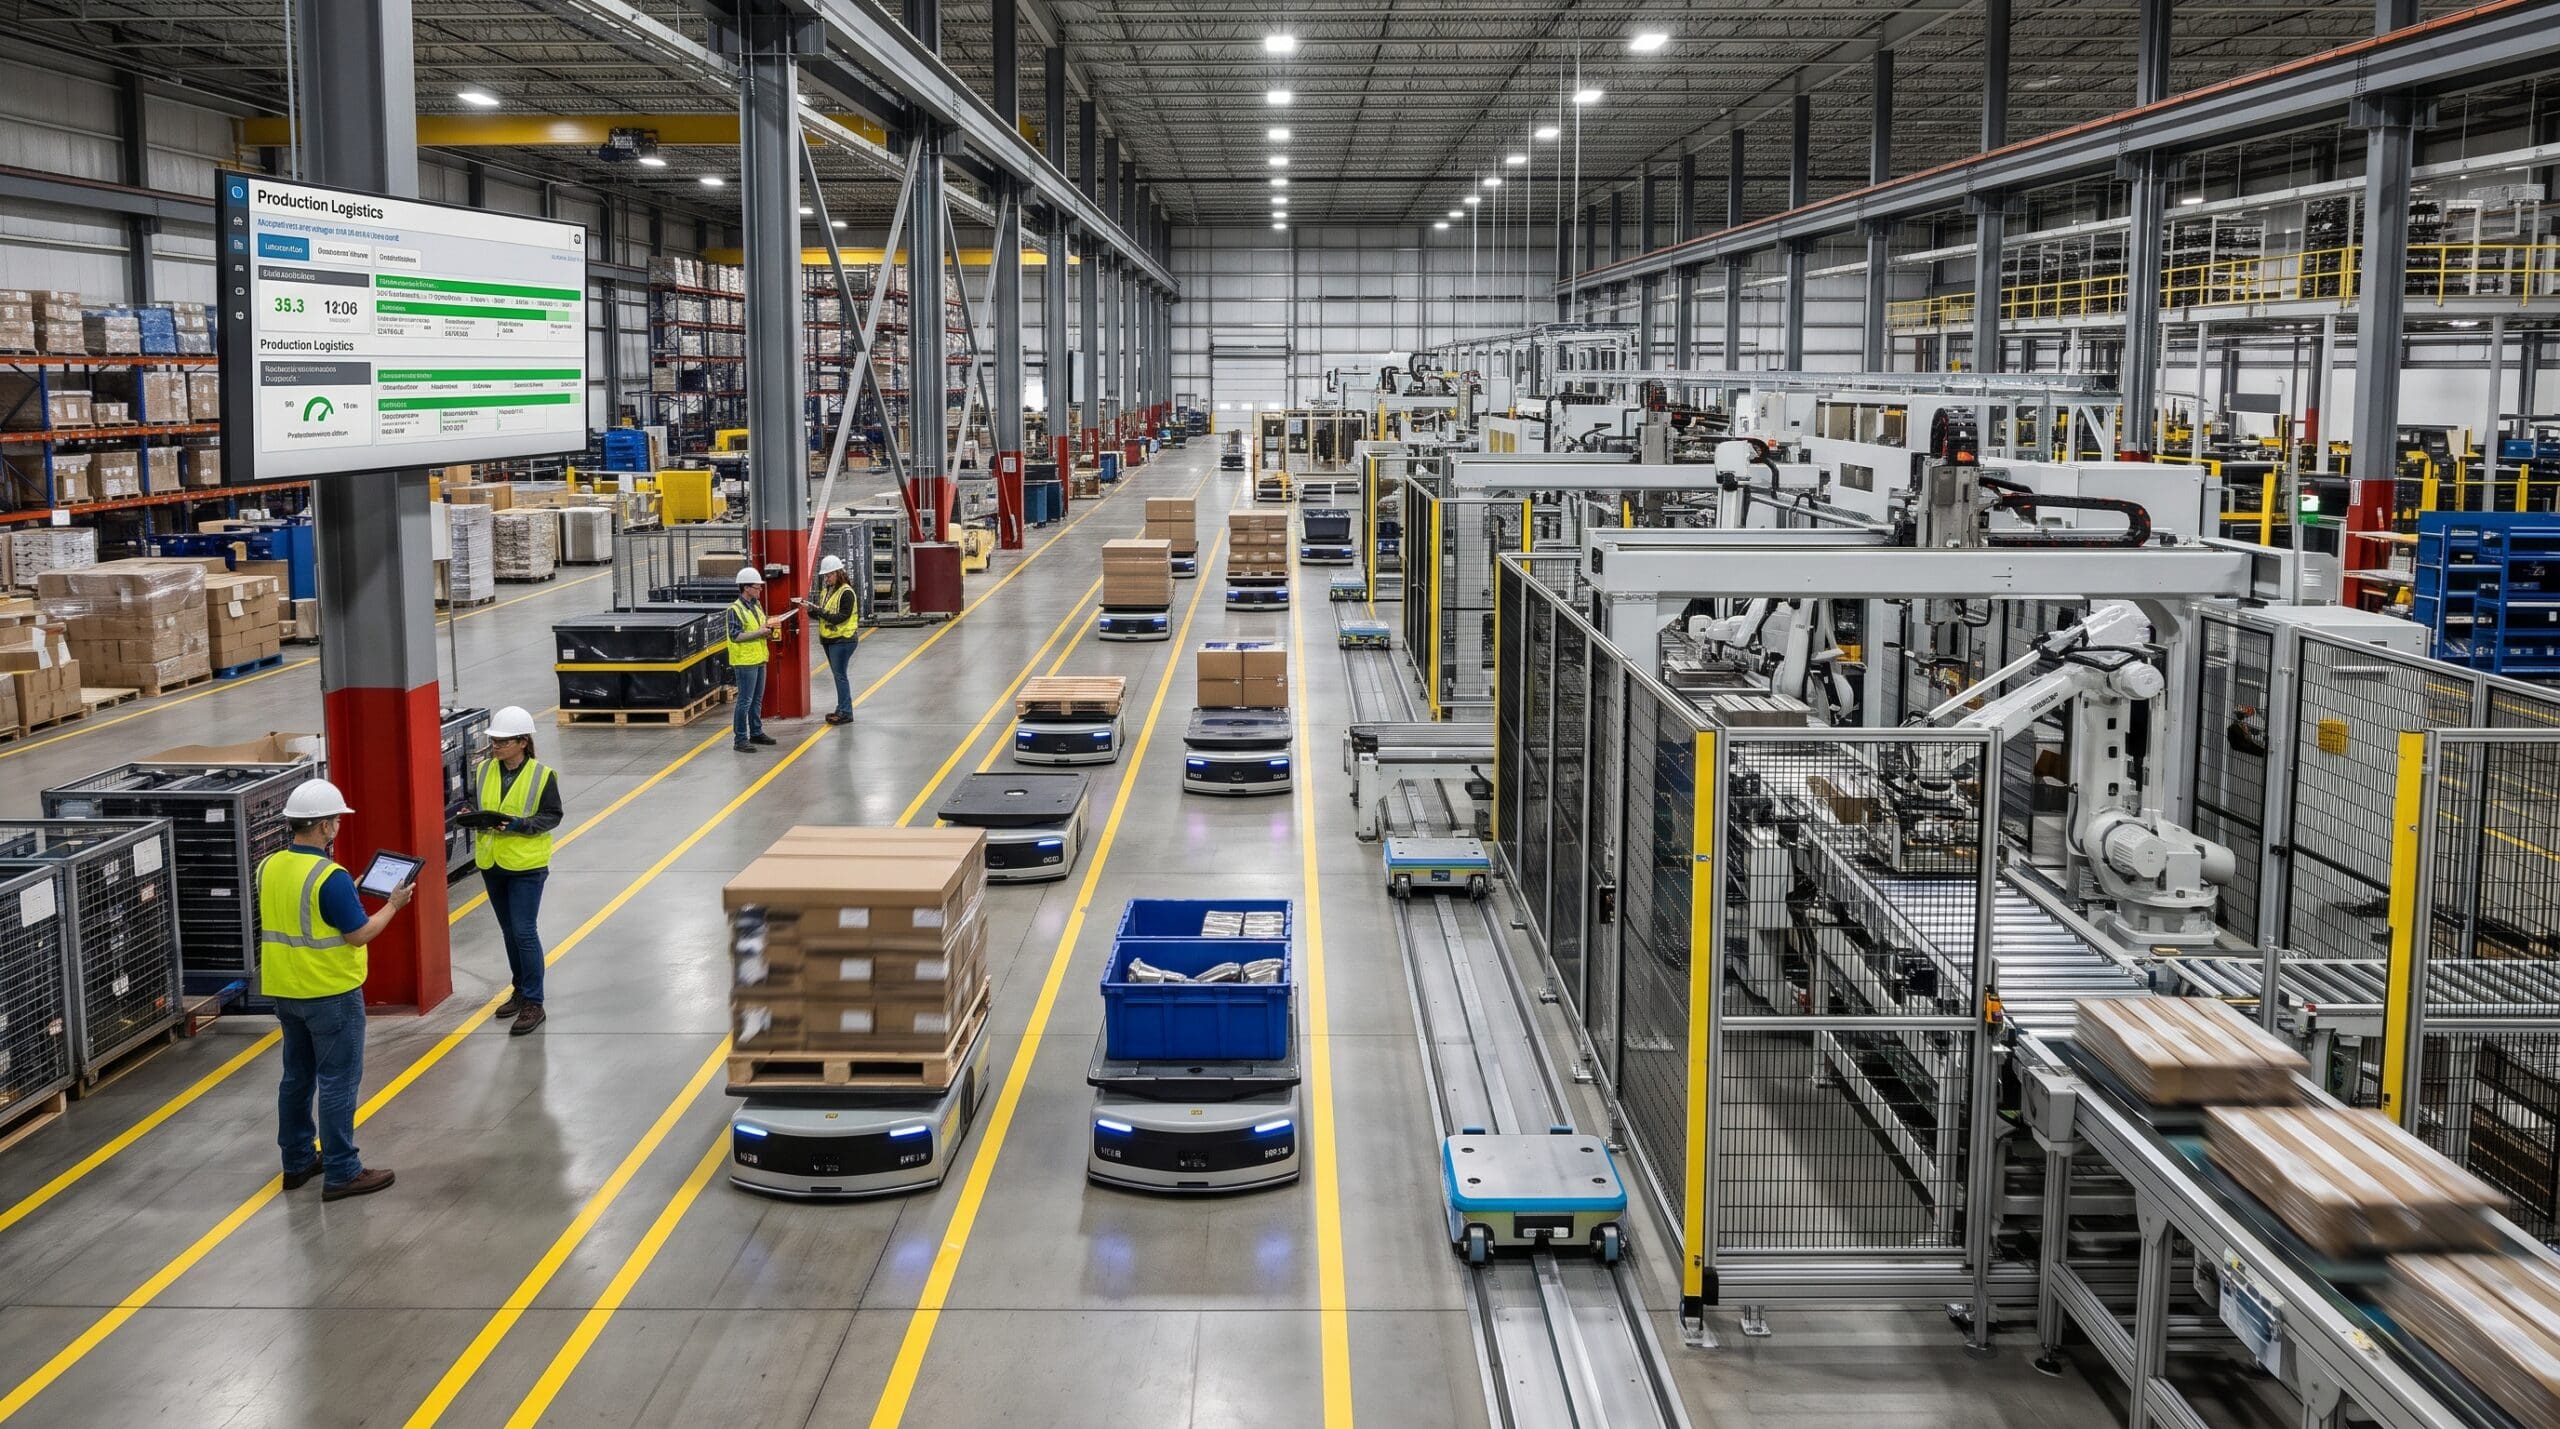
Rockwell Automation’s press conference presented a clear thesis: the next major productivity opportunity lies in the space between automated processes. Many factories have sophisticated machines and well-instrumented production lines, yet material still arrives through manual, disconnected workflows. The result is a familiar contradiction: a highly automated line can still depend on a forklift driver or an operator pushing a cart at its boundary.
“At the end of the line, there was a person driving a forklift and a person pushing a cart.”
That gap is where Rockwell is positioning production logistics. Rather than treating intralogistics as a stand-alone robotics project, the company describes an end-to-end workflow spanning production software, orchestration, controls, autonomous mobile robots, independent cart technology, and human work. This is a stronger industrial proposition than simply adding AMRs to a fleet. It treats the movement of work-in-process, components, packaging, and finished goods as part of the production system itself.
For manufacturers, the implication is significant. Material movement can become event-driven by production demand, quality status, inventory availability, and equipment conditions. The operational objective shifts from “dispatch a robot” to “maintain the production plan.”
From connected operations to autonomous response
Rockwell placed production logistics within a broader progression from connected operations to predictive and increasingly autonomous plants. Its “sense, think, act” framing is familiar in robotics, but the company extends the concept beyond the mobile robot to machines, lines, and plant-level workflows. Sensors establish context, software evaluates conditions, and physical assets execute the response, with a human retained in the loop where risk or uncertainty requires oversight.
“The right product to the right spot at the right time.”
This framing addresses one of the hardest problems in plant automation: local optimization does not automatically create system optimization. A packaging machine can be highly efficient while waiting for film. An assembly cell can meet its cycle time but starve because a component was not replenished in sequence. A warehouse can optimize picks while production priorities have already changed. The value of autonomy therefore depends on coordinating decisions across the workflow, not maximizing the utilization of each asset in isolation.
Rockwell’s stack: simulate, orchestrate, move
The press conference organized the production-logistics portfolio into three layers: simulation, orchestration, and movement. Together, these layers indicate how Rockwell intends to differentiate from robot-centric competitors and warehouse-only automation providers.
1. Simulate the operating model
Digital twins can validate layouts, traffic, throughput, safety zones, and control logic before equipment is commissioned. Rockwell also argued that major end users increasingly expect machine builders to provide a digital twin with the physical machine. In production logistics, that model has continuing value because routes, product mixes, cell configurations, and replenishment rules change over the asset lifecycle. A useful digital twin should therefore evolve from a commissioning tool into an operational decision-support asset.
2. Orchestrate work across people and assets
FactoryTalk Orchestration is central to the strategy. Rockwell said customer experience after its AMR acquisition revealed that the real challenge was coordinating robots with carts, people, machines, and software. That observation is directionally correct. Mixed environments will remain the norm for years, and manufacturers need workflow logic that can assign the next best task to an AMR, fixed system, or person while preserving production priorities.
The most compelling orchestration use case is dynamic response. If a supply-chain issue changes raw-material availability, the production schedule, material calls, and execution sequence should adjust together. This requires integration with manufacturing execution and production management systems, not merely fleet management.
3. Move material with the appropriate technology
Rockwell’s movement layer includes AMRs and independent cart technology, supplemented by robotics partners for applications such as palletizing. The portfolio reflects a practical reality: production logistics is not a single-robot category. Different workflows may require mobile transport, precise linear motion, storage and retrieval, or robotic handling. Competitive advantage will depend on coordinating these technologies as one workflow and integrating them to the control layer.
The Twinsburg case shows the value of integration
Rockwell used its Twinsburg, Ohio, plant as the principal proof point. The deployment began with autonomous material movement to reduce manual cart handling. The second phase integrated that capability with FactoryTalk production software, allowing the system to deliver the correct material in the required place, time, amount, and sequence.
According to the presentation, benefits from the first phase appeared in less than a month, while the interval between the first and second phases was approximately four to six months. Rockwell emphasized that workers were reassigned to higher-value plant roles rather than eliminated. The integrated phase reportedly reduced floor-space requirements and work-in-process, creating working-capital benefits in addition to labor-productivity gains.
“As soon as the pilot works, we immediately go to: how do we scale it across our facility?”
The case also illustrates an important adoption pattern. A transport-only pilot can establish safety, reliability, and workforce acceptance quickly. The larger business case emerges when the pilot is connected to production software and scaled across workflows. This is where manufacturers should measure schedule adherence, line starvation, work-in-process, floor-space consumption, indirect labor, and changeover performance, rather than focusing only on robot travel or labor displacement.
Manufacturing and warehousing are converging, but not becoming identical
Rockwell sees growing integration between production lines, adjacent warehouses, automated storage and retrieval systems, and shipping docks. Co-located manufacturing and warehousing make this convergence especially visible: components move from storage to assembly, finished goods move from the line to storage, and production priorities influence downstream handling.
However, Rockwell’s strongest position remains production logistics rather than general e-commerce fulfillment. The company can connect manufacturing software and controls to physical movement, whereas fulfillment specialists often optimize high-volume picking and seasonal labor flexibility. In warehouse environments, Rockwell must also integrate with warehouse management and warehouse execution systems. That makes interoperability, APIs, and ownership of workflow decisions crucial architectural questions.
Truck loading and unloading remain an important boundary. Rockwell described these applications as technically difficult because trailers vary, loads shift, and safety conditions are less controlled. This is a useful reminder that autonomous material flow will advance unevenly. Structured, repeatable movement inside the plant will automate faster than variable dock-edge work.
What manufacturers should do now
Start with a production constraint, not a robot count. Select a workflow where material availability affects throughput, such as line-side replenishment, packaging-material delivery, work-in-process transfer, or finished-goods evacuation. Define the baseline using line-starvation minutes, replenishment response time, indirect travel, and WIP.
Design the integration before the pilot. Document interfaces to MES or production management, ERP, WMS/WES, controls, safety systems, and identity services. A pilot that cannot exchange production status and task priorities may prove navigation but will not prove production value.
Model the mixed environment. Assume people, forklifts, carts, AMRs, conveyors, and fixed automation will coexist. Validate traffic, exceptions, manual recovery, charging, and safe-state behavior using a digital model before scaling.
Use phased economics. Separate phase-one transport savings from phase-two operational gains. The latter may include lower WIP, recovered floor space, better sequence adherence, fewer shortages, and higher OEE. These benefits often justify integration effort more than labor savings alone.
Build change management into commissioning. Create role-specific training for operators, maintenance, supervisors, controls engineers, and IT/OT teams. Define who owns workflow rules, exception handling, fleet availability, cybersecurity, and continuous improvement.
Analyst assessment
Rockwell’s production-logistics message is strategically credible because it aligns with the company’s installed base and its ability to integrate software, controls, motion, and robotics. The acquisition of an AMR platform supplied a visible physical asset, but orchestration is the more consequential layer. If Rockwell can make FactoryTalk Orchestration open enough to coordinate heterogeneous equipment and straightforward enough for plants to deploy repeatedly, it can compete for a broader share of the intralogistics architecture.
Execution risks remain. Manufacturers operate mixed fleets and multiple software systems, so closed or overly Rockwell-centric workflows would limit adoption. Digital-twin value also depends on maintaining models after commissioning, a discipline many plants have not established. Finally, the ROI claims in the transcript include several partially captured figures; buyers should request validated baselines, calculation methods, and comparable references before generalizing the Twinsburg results.
The larger trend is clear: production logistics is moving from an indirect support function toward a software-defined component of plant operations. The winners will not be determined only by the best mobile robot. They will be the suppliers that connect material movement to production intent, manage exceptions across people and machines, and turn successful pilots into repeatable plant-wide operating models.
The post Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy appeared first on Logistics Viewpoints.

When One Character Stops the Workflow: The Hidden Digital Dependencies of Modern Supply Chains
Always-On AI Is Coming to Supply Chains. But Who Owns the Exception?

Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy
Freightos Global Freight Outlook – September 2026
Container rates jump another $1k/FEU – but is demand peaking? – July 8, 2026 Update

Walmart and the New Supply Chain Reality: AI, Automation, and Resilience
Trending
- Non classé3 mois ago
Freightos Global Freight Outlook – September 2026
- Non classé5 mois ago
Container rates jump another $1k/FEU – but is demand peaking? – July 8, 2026 Update
-
 Non classé2 ans ago
Walmart and the New Supply Chain Reality: AI, Automation, and Resilience
-
 Non classé7 mois ago
Why Sulfuric Acid Is Emerging as a Supply Chain Constraint in Copper
- Non classé6 mois ago
Container rates starting to spike on peak season rush – June 2, 2026 Update
- Non classé1 an ago
13 Books Logistics And Supply Chain Experts Need To Read
- Non classé1 an ago
Ex-Asia ocean rates climb on GRIs, despite slowing demand – October 22, 2025 Update
- Non classé5 mois ago
LCL Shipping Cost Calculator: Calculate Air and Sea Shipping Freight Rates