Non classé
Oil and Gas Electrification and Automation: Modernizing Field Logistics and Operations

Published
5 mois agoon
By
Electrification and automation in oil and gas are often discussed through the lens of decarbonization. That lens is important, but it is incomplete. For supply chain and operations leaders, these technologies should be evaluated as modernization tools that reshape how field operations, terminals, refineries, warehouses, pipelines, and support fleets are powered, monitored, maintained, and coordinated.
Oil and Gas in the Supply Chain: A Strategic Framework for Building Resilient and Responsible Supply Chains.
The practical question is not whether an asset can be electrified or automated. The better question is whether the change improves supply chain performance. Does it reduce downtime? Does it improve field visibility? Does it lower maintenance intensity? Does it reduce hazardous work? Does it create better data for planning and control? Does it improve resilience rather than add another point of failure?
That operating lens matters because oil and gas supply chains are not uniform. A grid-connected basin, an offshore platform, a refinery warehouse, a marine terminal, and a remote pipeline station all have different duty cycles, infrastructure constraints, power requirements, safety profiles, and logistics needs. Electrification and automation create value when they are applied selectively, sequenced appropriately, and tied to defined operational outcomes.
Electrification Is a System Design Decision
Electrification is sometimes described as a straightforward equipment replacement exercise: remove diesel-powered equipment and install electric alternatives. In reality, it is a broader system design decision. It changes the requirements for infrastructure, power reliability, maintenance planning, workforce skills, emergency response, operating procedures, capital allocation, and digital control.
An electrified field operation depends on much more than the equipment itself. It requires adequate power availability, load management, backup power, grid access, on-site generation where needed, battery storage, and control systems that can coordinate demand. If power is unreliable, poorly managed, or insufficient for peak operating needs, electrification can introduce new operational vulnerability. If power is reliable, resilient, and digitally managed, electrification can improve cost performance, uptime, emissions performance, and asset visibility.
This is why electrification belongs in the supply chain strategy rather than in a standalone sustainability workstream. The decision affects field logistics, maintenance scheduling, spare parts strategies, contractor requirements, safety procedures, and contingency planning. It also changes the data environment. Electrified assets can often generate more consistent operational data, which can feed maintenance systems, planning tools, and control towers.
Where Electrification Makes Supply Chain Sense
The strongest near-term opportunities are typically found in operations with predictable duty cycles, concentrated assets, and controllable infrastructure. These are the environments where the operational case can be evaluated with discipline and where infrastructure investment can be matched to actual use patterns.
Examples include electric drilling rigs in grid-connected basins, electric compressors and pumps, electric terminal equipment, warehouse forklifts, electric yard tractors, battery-powered inspection drones, electric maintenance vehicles, electrified pipeline pump stations, shore power at marine terminals, and battery-supported remote operations. In these settings, the business case may include lower fuel consumption, fewer maintenance events, improved safety, better utilization data, and reduced exposure to fuel logistics disruptions.
However, electrification should not become a generic mandate. Oil and gas assets vary significantly by location, power access, operational criticality, and load profile. A remote site with limited power redundancy may require a very different approach than a refinery complex with substantial electrical infrastructure. A high-utilization terminal fleet may justify charging infrastructure more readily than a low-duty-cycle support vehicle fleet. The right strategy is selective and staged.
Supply chain leaders should therefore ask a set of practical questions before committing capital. What operational constraint is being solved? What power infrastructure is required? What happens during an outage? How will load be prioritized? What maintenance capabilities are needed? What data will be created, and how will it be used? How does the change affect contractors, inventory, safety, and emergency response?
Field Logistics Remains a High-Value Modernization Target
Field logistics is one of the most complex segments of the oil and gas supply chain. It often involves remote locations, specialized contractors, hazardous materials, variable demand, weather exposure, limited infrastructure, and significant safety risk. The traditional operating model still relies heavily on phone calls, spreadsheets, manual dispatch, paper field tickets, and fragmented contractor systems.
That fragmentation creates cost and risk. Crews wait for materials. Equipment moves inefficiently. Contractors operate with incomplete visibility. Maintenance work is delayed because the required parts, permits, people, or vehicles are not synchronized. In volatile operating environments, these delays can affect production reliability and safety performance.
Digital field logistics modernization can reduce this friction. Digital dispatch, route optimization, contractor visibility, mobile field applications, digital field tickets, materials tracking, drone inspection, remote monitoring, automated replenishment, and integrated maintenance planning all improve the ability to coordinate work in the field. The value is not limited to transportation cost reduction. It includes fewer wasted moves, better safety controls, improved schedule adherence, more reliable production support, and better data for decision-making.
Modern field logistics also improves the connection between planning and execution. When field activity is captured digitally, companies can better understand recurring demand, contractor performance, parts consumption, route constraints, asset condition, and the true cost of supporting dispersed operations. This information can then inform network design, stocking policies, maintenance strategies, and capital planning.
Automation Turns Workflows into Data Streams
Automation and robotics are expanding across oil and gas operations because many field activities are difficult, dangerous, repetitive, or inspection-intensive. Pipeline inspection, tank inspection, offshore facility inspection, methane detection, flare monitoring, warehouse automation, valve inspection, terminal monitoring, security patrols, and hazardous area inspection are all strong use cases.
The value of automation is not simply labor substitution. In many cases, the more important benefit is improved visibility into assets and flows. Robots, drones, sensors, and autonomous systems can collect structured data more consistently than manual processes. That data can feed maintenance management systems, emissions platforms, digital twins, asset performance systems, and supply chain control towers.
This changes the operating model. A tank inspection is no longer just a task completed by a person or machine. It becomes a data-generating workflow that can be analyzed, compared, trended, and linked to maintenance planning. A drone inspection of a pipeline or terminal can reduce human exposure while also improving the timeliness and quality of condition data. Automated warehouse systems can improve accuracy and throughput while generating better inventory and labor visibility.
For supply chain leaders, this means automation should be evaluated not only by the direct cost of the task being automated, but also by the downstream value of the data created. Better inspection data can reduce unplanned downtime. Better inventory data can reduce emergency orders. Better asset condition data can improve maintenance planning. Better field visibility can improve contractor coordination and safety.
Total Cost of Ownership Is the Right Business Case
Electrification and automation require a total cost of ownership view. Equipment acquisition cost is only one part of the calculation. The business case should also consider infrastructure cost, power or fuel savings, maintenance savings, asset uptime, safety improvements, emissions value, training requirements, operating flexibility, residual value, and potential regulatory benefits.
In many cases, the strongest justification will not be a simple energy cost comparison. The more compelling case may be higher reliability, fewer maintenance interventions, lower operational risk, better data, and improved ability to coordinate field activity. These benefits are especially important in oil and gas, where downtime, safety incidents, and emergency logistics can be far more expensive than routine operating costs suggest.
A total cost approach also helps avoid poorly sequenced investments. Buying electric equipment before the power and control infrastructure is ready can create performance problems. Deploying robotics without integrating the inspection data into maintenance systems can limit value. Automating a warehouse process without addressing inventory accuracy and master data may produce disappointing results. Modernization works best when technology, process, workforce, and infrastructure are designed together.
Workforce, Cybersecurity, and Resilience Cannot Be Afterthoughts
Electrification and automation change workforce requirements. Oil and gas companies will need deeper capabilities in high-voltage safety, electrical maintenance, sensor diagnostics, remote operations, robotics support, data interpretation, operational technology cybersecurity, and digital workflow management. These skills must be planned, trained, and embedded into operating procedures.
Resilience is equally important. Electrified assets depend on power continuity. Automated systems depend on connectivity, controls, and cybersecurity. Backup power, battery storage, manual override procedures, redundant communications, load prioritization, emergency operating procedures, and high-voltage safety protocols must be part of the design from the beginning.
The goal is not to make operations more technologically impressive. The goal is to make them more reliable, safer, more visible, and more controllable. Modernization should reduce fragility, not introduce it. That requires cross-functional governance across operations, supply chain, engineering, IT, OT, maintenance, safety, and finance.
The Supply Chain Leadership Imperative
Oil and gas companies have an opportunity to use electrification and automation to modernize the supply chain from the field to the terminal and from the warehouse to the control room. The winners will not be those that deploy the most technology. They will be those that align technology with duty cycles, infrastructure readiness, field logistics realities, workforce capability, and resilience requirements.
For supply chain executives, the mandate is clear: treat electrification and automation as operating model decisions. Tie investments to measurable outcomes. Build the power, data, maintenance, and safety foundations. Sequence adoption by use case and operational readiness. And ensure that every modernization initiative improves the performance of the broader supply chain.
To explore the broader implications for oil and gas supply chain strategy, Download the full ARC Advisory Group white paper.
Download Oil and Gas in the Supply Chain.
The post Oil and Gas Electrification and Automation: Modernizing Field Logistics and Operations appeared first on Logistics Viewpoints.
You may like
Non classé
Always-On AI Is Coming to Supply Chains. But Who Owns the Exception?
Published
17 heures agoon
21 novembre 2026By
The supply chain industry has invested heavily in detecting problems sooner. Transportation visibility systems identify late shipments, planning applications flag shortages, and control towers consolidate operational alerts. Yet knowing about an exception and resolving it are two different things. The delay may be visible to everyone, while responsibility for the next action remains surprisingly unclear.
That gap is becoming more important as artificial intelligence moves beyond answering questions and begins maintaining responsibility for work over time. On November 19, OpenAI expanded access to ChatGPT Dots, its persistent agents, to eligible ChatGPT Business Standard users, while testing access with a limited group of Plus subscribers. The agents can retain useful context, work with authorized applications, and pursue continuing assignments. This is not the same as releasing an autonomous transportation management system. It does, however, point toward an operating model that supply chain leaders should be examining.
The critical question is not whether an AI agent can produce a better recommendation. It is whether an organization can assign a bounded operational responsibility, know who is accountable for the result, and verify that the work was actually completed.
The Supply Chain Has an Execution Gap
Consider how many logistics exceptions are managed today. A late container generates an alert. A transportation planner checks the revised estimated arrival, calls the carrier, and coordinates with a distribution center. Someone may approve a new receiving window or an inventory transfer. But the work does not end when the recommendation is accepted. The carrier must acknowledge the change, the appointment must be updated, and the revised plan must hold up as conditions change.
A great deal of operational effort is spent in the intervals between those actions. Employees chase confirmations, reconstruct previous conversations, and determine whether an apparent resolution was reflected in the system of record. Enterprise applications support the process, but they do not always maintain a single durable record of who owns the exception through closure.
Persistent AI could improve this situation by preserving the case history, recognizing when new information changes its significance, and continuing to monitor outstanding actions. The benefit is not simply an answer that arrives in seconds. It is potentially less time between identifying an exception, deciding what to do, and confirming that the decision produced the intended operational result.
A New Class of Agents, Not a New TMS
The foundation-model providers are approaching persistent work from different directions. OpenAI’s Dots emphasize ongoing assignments supported by connected applications and dedicated computing environments. Anthropic’s Claude Managed Agents provide infrastructure for long-running, bounded execution, including retained state, tool controls, and scheduled activity. Google’s Gemini enterprise initiatives emphasize organizational integration, permissions, and governance. xAI’s Grok Bot 1.0 emphasizes collaborative agents that can recognize unfinished team activities and follow up.
These are different products with different degrees of maturity and integration. Their common direction is more important than their marketing similarities: AI is progressing from episodic interaction toward sustained work. None should be assumed capable of managing production-critical logistics transactions without appropriate enterprise architecture, validated integrations, and operational controls.
That distinction matters. Scheduled research, monitoring an inbox, retrieving shipment status, changing an appointment, and committing a freight expenditure are not interchangeable capabilities. As autonomy increases, the required standard for identity, data quality, permissions, auditability, and error recovery increases with it.
Follow the Exception to Its Actual Conclusion
Imagine a retailer with an inbound shipment of promotional merchandise approaching a regional distribution center. A visibility system reports a delay. The TMS holds carrier and shipment information, the WMS manages receiving capacity, and the ERP and order systems establish inventory requirements and customer commitments. The immediate question is whether the revised arrival threatens service or creates avoidable cost.
An AI agent assigned to investigate could gather those inputs, compare alternatives, and prepare a recommended receiving or fulfillment plan. As the arrival estimate changes, it could retain what was previously considered, which assumptions remain valid, and which decisions are pending. That continuity avoids repeatedly starting the investigation from scratch.
But the more important test comes after a planner approves a different receiving appointment. Was the carrier notified? Did it accept the arrangement? Was the appointment changed in the authoritative scheduling system? Did the warehouse have the promised capacity? If a later delay invalidated the plan, did the exception reopen and reach the right person?
An agent that offers an excellent recommendation and then loses track of its execution has not closed the exception. It has shifted the remaining work to someone else. The opportunity for persistent AI is to keep that bounded responsibility visible until the required evidence of completion exists, while escalating decisions that exceed its authority.
Assign the Work Without Surrendering Accountability
In a recent Logistics Viewpoints discussion of who controls the supply chain’s AI decision layer, I examined the competition among model providers, enterprise application vendors, and orchestration platforms. Ownership of the decision architecture is one question. Ownership of the work following a decision is another. An enterprise can have powerful optimization capabilities and still struggle with incomplete handoffs.
This argues for a straightforward operating discipline. Every persistent exception should have an identified business owner, a responsible workflow or agent, a defined next action, a deadline or reassessment trigger, an escalation path, and explicit closure criteria. Those attributes should be held in durable case state, with references back to authoritative records. They cannot depend solely on a model’s conversational memory.
I would also separate three levels of authority. Observation permits an agent to retrieve data, compare conditions, and monitor progress. Recommendation permits it to propose a response for approval. Execution permits it to modify records or commit resources, and should require controls proportionate to the financial and operational consequences. A carrier appointment change, an inventory allocation, and a customer delivery promise may require different approval rules even when they originate from the same exception.
Protocols such as Model Context Protocol and agent-to-agent messaging can simplify access and coordination. They do not, by themselves, create a durable operational record, verify transactions, or resolve the question of business accountability. The architecture must still reconcile agent activity with what the TMS, WMS, ERP, and other systems of record actually show.
The Economic Test Is the Resolved Case
Executives should resist measuring persistent AI by the number of tasks performed, messages generated, or hours an agent appears to be active. An agent that repeatedly checks shipment status without changing an outcome can create additional cost while adding little value. The relevant economic unit is the satisfactorily resolved exception.
Consider an illustrative transportation organization handling 200 exceptions per week. If better investigation and follow-up release an average of 15 minutes of manual effort per case, that represents 50 gross staff hours weekly. It is a useful starting estimate, not a verified savings figure. Human review, failed attempts, integration expenses, model usage, and oversight must be included before calculating net return.
More consequential gains may come from avoiding an expedited shipment, reducing detention, preventing a production interruption, or protecting a customer commitment. A credible pilot should therefore measure time to assessment, time awaiting approval, time to verified completion, reopened cases, intervention rates, and the total cost per resolved exception. These measures distinguish productive persistence from continuous activity.
Start with Work That Repeatedly Stalls
The best initial candidates are information-intensive processes requiring repeated follow-up but limited transaction authority: delayed inbound loads, supplier confirmations, purchase order discrepancies, inventory shortages, and customer order escalations. Select one exception category, establish its closure criteria, and compare agent-supported handling with the current process across the full life of each case.
The evaluation should include changed arrival times, missing data, unavailable integrations, competing priorities, and handoffs between employees. It should also establish when the agent must stop, ask for approval, or return control to a human operator. Successful demonstrations are less important than dependable behavior when the process becomes messy.
AI’s progression toward always-on work is significant, but it should not be confused with a near-term transition to fully autonomous supply chains. The harder problem remains coordinating people, processes, technology, and decision rights across the enterprise. The most valuable agent may not be the one that first identifies a late shipment. It may be the one that helps the organization establish, with evidence, that the problem was actually resolved.
The post Always-On AI Is Coming to Supply Chains. But Who Owns the Exception? appeared first on Logistics Viewpoints.
Non classé
Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy
Published
2 jours agoon
20 novembre 2026By
An analyst perspective on why orchestration, digital twins, and plant-floor integration matter more than the robot alone
Production logistics becomes a control problem
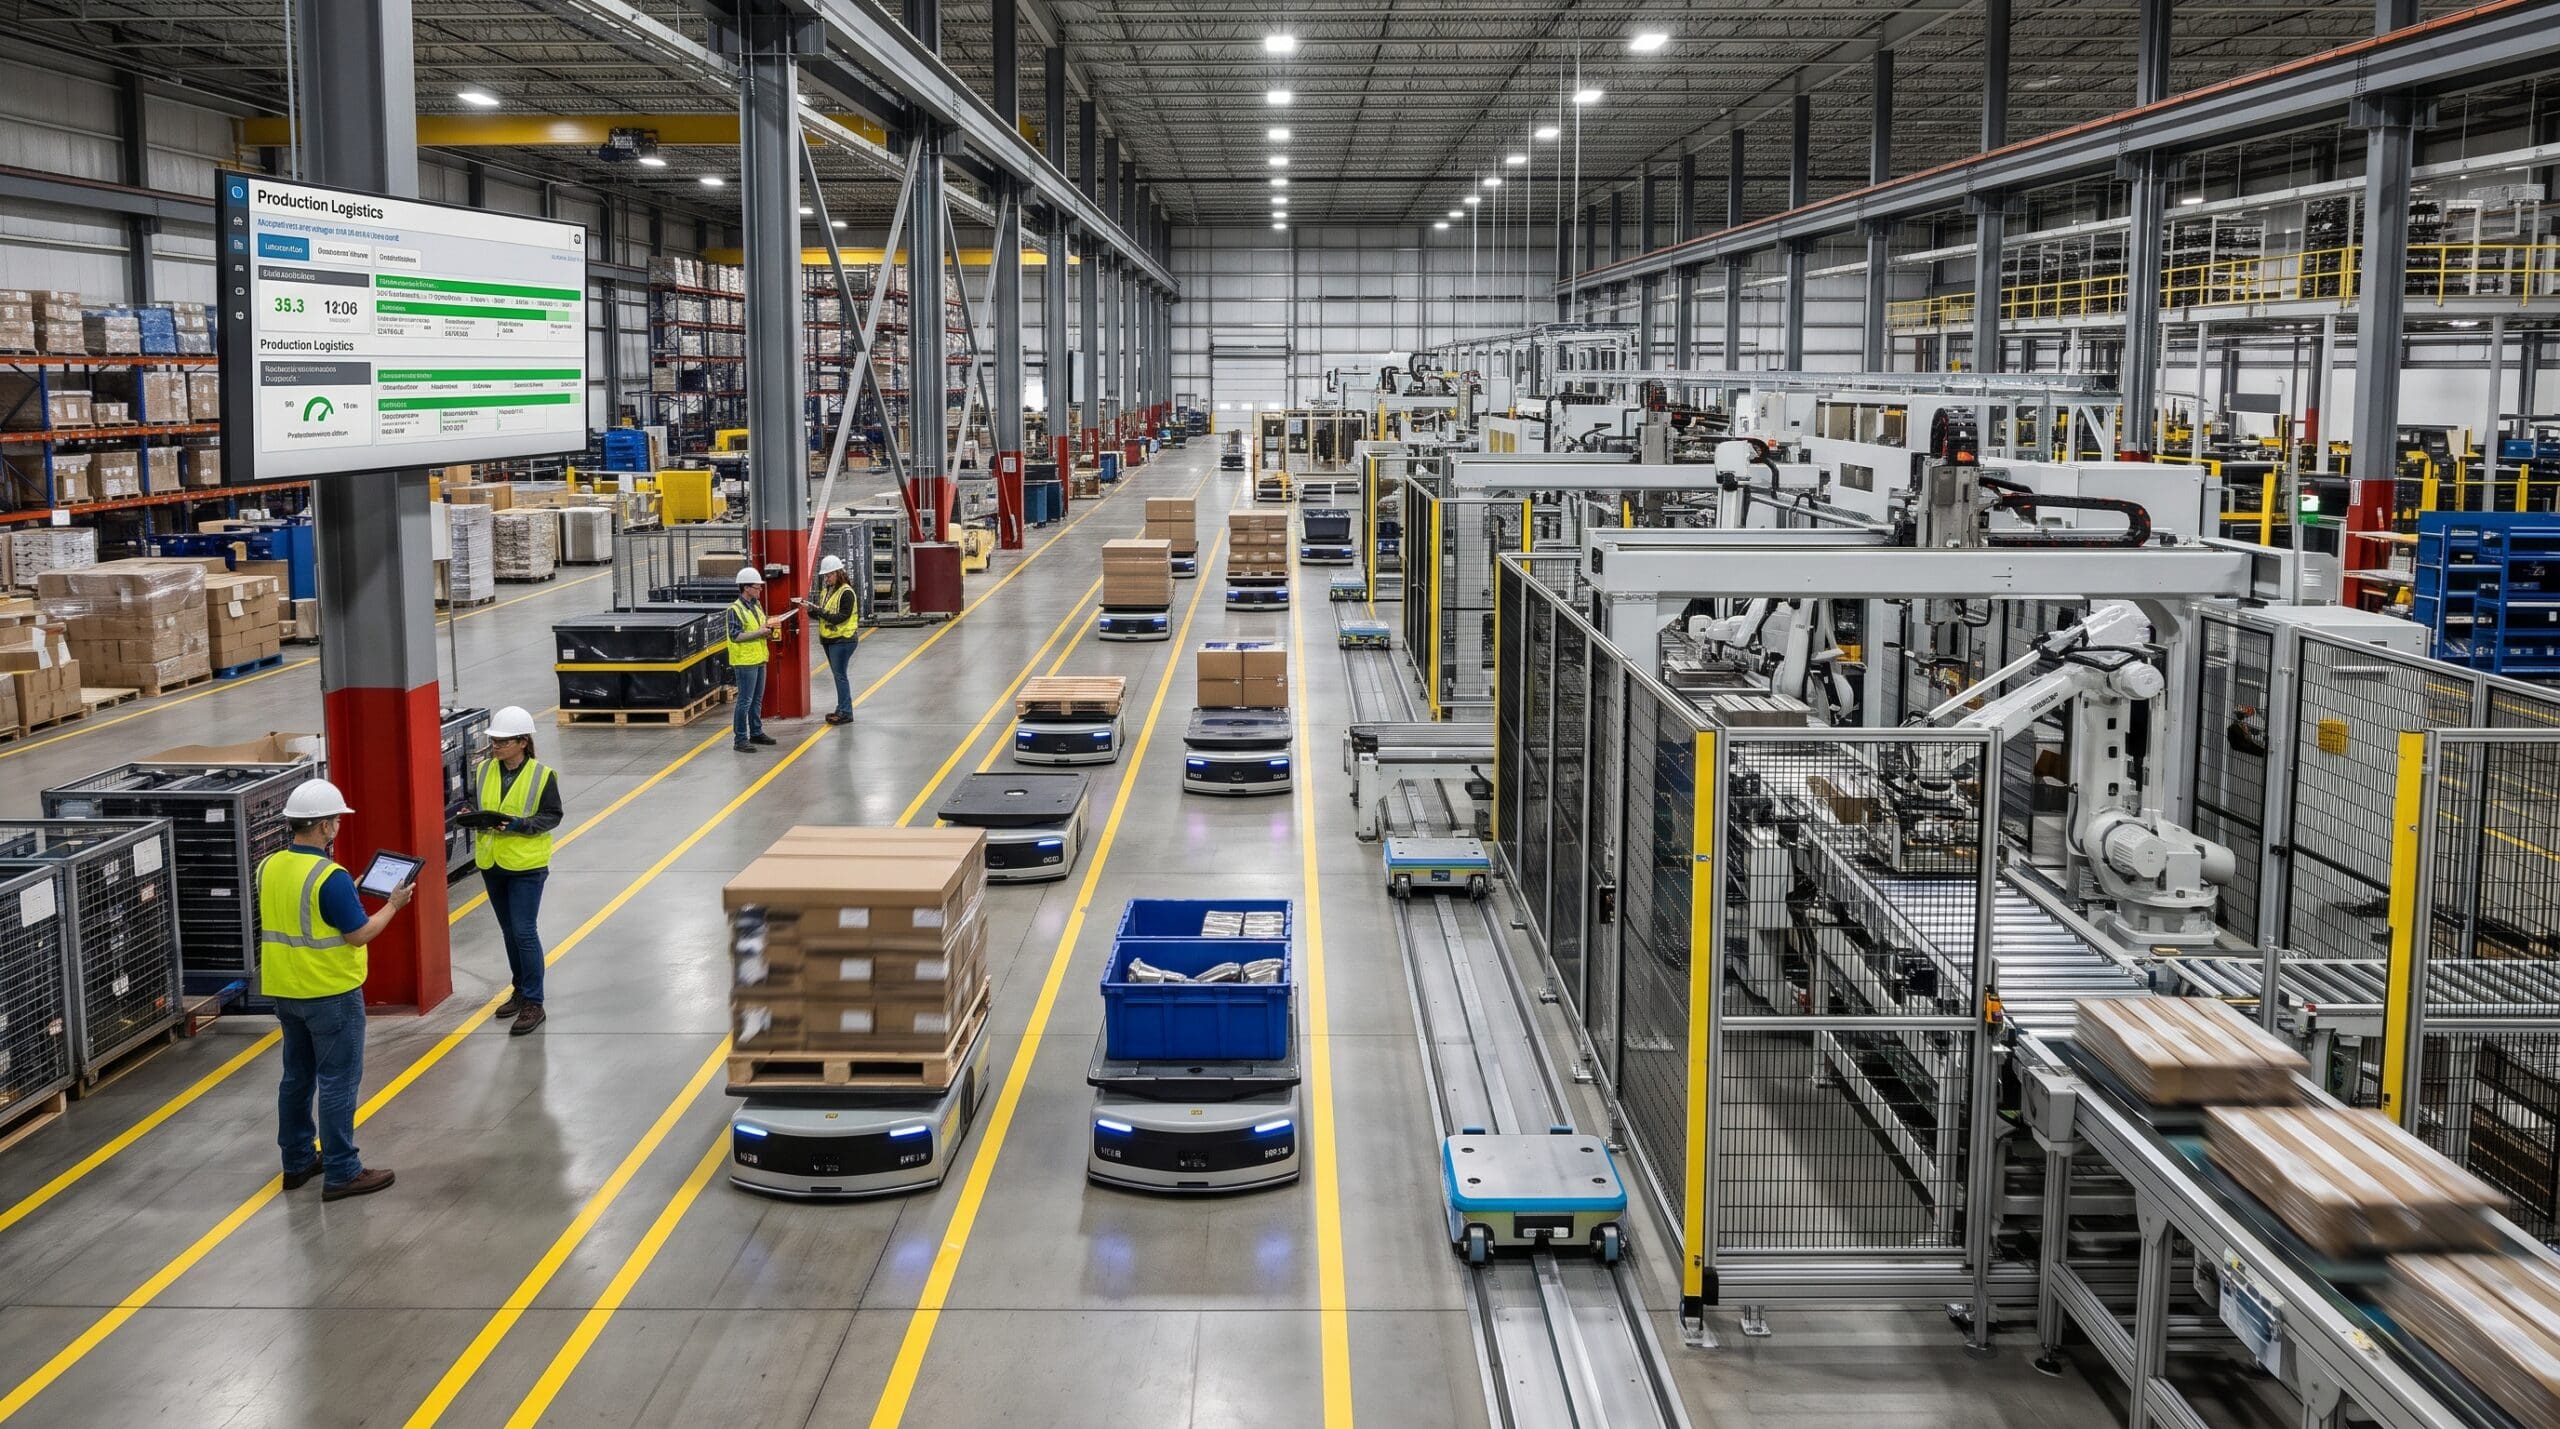
Rockwell Automation’s press conference presented a clear thesis: the next major productivity opportunity lies in the space between automated processes. Many factories have sophisticated machines and well-instrumented production lines, yet material still arrives through manual, disconnected workflows. The result is a familiar contradiction: a highly automated line can still depend on a forklift driver or an operator pushing a cart at its boundary.
“At the end of the line, there was a person driving a forklift and a person pushing a cart.”
That gap is where Rockwell is positioning production logistics. Rather than treating intralogistics as a stand-alone robotics project, the company describes an end-to-end workflow spanning production software, orchestration, controls, autonomous mobile robots, independent cart technology, and human work. This is a stronger industrial proposition than simply adding AMRs to a fleet. It treats the movement of work-in-process, components, packaging, and finished goods as part of the production system itself.
For manufacturers, the implication is significant. Material movement can become event-driven by production demand, quality status, inventory availability, and equipment conditions. The operational objective shifts from “dispatch a robot” to “maintain the production plan.”
From connected operations to autonomous response
Rockwell placed production logistics within a broader progression from connected operations to predictive and increasingly autonomous plants. Its “sense, think, act” framing is familiar in robotics, but the company extends the concept beyond the mobile robot to machines, lines, and plant-level workflows. Sensors establish context, software evaluates conditions, and physical assets execute the response, with a human retained in the loop where risk or uncertainty requires oversight.
“The right product to the right spot at the right time.”
This framing addresses one of the hardest problems in plant automation: local optimization does not automatically create system optimization. A packaging machine can be highly efficient while waiting for film. An assembly cell can meet its cycle time but starve because a component was not replenished in sequence. A warehouse can optimize picks while production priorities have already changed. The value of autonomy therefore depends on coordinating decisions across the workflow, not maximizing the utilization of each asset in isolation.
Rockwell’s stack: simulate, orchestrate, move
The press conference organized the production-logistics portfolio into three layers: simulation, orchestration, and movement. Together, these layers indicate how Rockwell intends to differentiate from robot-centric competitors and warehouse-only automation providers.
1. Simulate the operating model
Digital twins can validate layouts, traffic, throughput, safety zones, and control logic before equipment is commissioned. Rockwell also argued that major end users increasingly expect machine builders to provide a digital twin with the physical machine. In production logistics, that model has continuing value because routes, product mixes, cell configurations, and replenishment rules change over the asset lifecycle. A useful digital twin should therefore evolve from a commissioning tool into an operational decision-support asset.
2. Orchestrate work across people and assets
FactoryTalk Orchestration is central to the strategy. Rockwell said customer experience after its AMR acquisition revealed that the real challenge was coordinating robots with carts, people, machines, and software. That observation is directionally correct. Mixed environments will remain the norm for years, and manufacturers need workflow logic that can assign the next best task to an AMR, fixed system, or person while preserving production priorities.
The most compelling orchestration use case is dynamic response. If a supply-chain issue changes raw-material availability, the production schedule, material calls, and execution sequence should adjust together. This requires integration with manufacturing execution and production management systems, not merely fleet management.
3. Move material with the appropriate technology
Rockwell’s movement layer includes AMRs and independent cart technology, supplemented by robotics partners for applications such as palletizing. The portfolio reflects a practical reality: production logistics is not a single-robot category. Different workflows may require mobile transport, precise linear motion, storage and retrieval, or robotic handling. Competitive advantage will depend on coordinating these technologies as one workflow and integrating them to the control layer.
The Twinsburg case shows the value of integration
Rockwell used its Twinsburg, Ohio, plant as the principal proof point. The deployment began with autonomous material movement to reduce manual cart handling. The second phase integrated that capability with FactoryTalk production software, allowing the system to deliver the correct material in the required place, time, amount, and sequence.
According to the presentation, benefits from the first phase appeared in less than a month, while the interval between the first and second phases was approximately four to six months. Rockwell emphasized that workers were reassigned to higher-value plant roles rather than eliminated. The integrated phase reportedly reduced floor-space requirements and work-in-process, creating working-capital benefits in addition to labor-productivity gains.
“As soon as the pilot works, we immediately go to: how do we scale it across our facility?”
The case also illustrates an important adoption pattern. A transport-only pilot can establish safety, reliability, and workforce acceptance quickly. The larger business case emerges when the pilot is connected to production software and scaled across workflows. This is where manufacturers should measure schedule adherence, line starvation, work-in-process, floor-space consumption, indirect labor, and changeover performance, rather than focusing only on robot travel or labor displacement.
Manufacturing and warehousing are converging, but not becoming identical
Rockwell sees growing integration between production lines, adjacent warehouses, automated storage and retrieval systems, and shipping docks. Co-located manufacturing and warehousing make this convergence especially visible: components move from storage to assembly, finished goods move from the line to storage, and production priorities influence downstream handling.
However, Rockwell’s strongest position remains production logistics rather than general e-commerce fulfillment. The company can connect manufacturing software and controls to physical movement, whereas fulfillment specialists often optimize high-volume picking and seasonal labor flexibility. In warehouse environments, Rockwell must also integrate with warehouse management and warehouse execution systems. That makes interoperability, APIs, and ownership of workflow decisions crucial architectural questions.
Truck loading and unloading remain an important boundary. Rockwell described these applications as technically difficult because trailers vary, loads shift, and safety conditions are less controlled. This is a useful reminder that autonomous material flow will advance unevenly. Structured, repeatable movement inside the plant will automate faster than variable dock-edge work.
What manufacturers should do now
Start with a production constraint, not a robot count. Select a workflow where material availability affects throughput, such as line-side replenishment, packaging-material delivery, work-in-process transfer, or finished-goods evacuation. Define the baseline using line-starvation minutes, replenishment response time, indirect travel, and WIP.
Design the integration before the pilot. Document interfaces to MES or production management, ERP, WMS/WES, controls, safety systems, and identity services. A pilot that cannot exchange production status and task priorities may prove navigation but will not prove production value.
Model the mixed environment. Assume people, forklifts, carts, AMRs, conveyors, and fixed automation will coexist. Validate traffic, exceptions, manual recovery, charging, and safe-state behavior using a digital model before scaling.
Use phased economics. Separate phase-one transport savings from phase-two operational gains. The latter may include lower WIP, recovered floor space, better sequence adherence, fewer shortages, and higher OEE. These benefits often justify integration effort more than labor savings alone.
Build change management into commissioning. Create role-specific training for operators, maintenance, supervisors, controls engineers, and IT/OT teams. Define who owns workflow rules, exception handling, fleet availability, cybersecurity, and continuous improvement.
Analyst assessment
Rockwell’s production-logistics message is strategically credible because it aligns with the company’s installed base and its ability to integrate software, controls, motion, and robotics. The acquisition of an AMR platform supplied a visible physical asset, but orchestration is the more consequential layer. If Rockwell can make FactoryTalk Orchestration open enough to coordinate heterogeneous equipment and straightforward enough for plants to deploy repeatedly, it can compete for a broader share of the intralogistics architecture.
Execution risks remain. Manufacturers operate mixed fleets and multiple software systems, so closed or overly Rockwell-centric workflows would limit adoption. Digital-twin value also depends on maintaining models after commissioning, a discipline many plants have not established. Finally, the ROI claims in the transcript include several partially captured figures; buyers should request validated baselines, calculation methods, and comparable references before generalizing the Twinsburg results.
The larger trend is clear: production logistics is moving from an indirect support function toward a software-defined component of plant operations. The winners will not be determined only by the best mobile robot. They will be the suppliers that connect material movement to production intent, manage exceptions across people and machines, and turn successful pilots into repeatable plant-wide operating models.
The post Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy appeared first on Logistics Viewpoints.
Non classé
Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy
Published
2 jours agoon
20 novembre 2026By
An analyst perspective on why orchestration, digital twins, and plant-floor integration matter more than the robot alone
Production logistics becomes a control problem
Rockwell Automation’s press conference presented a clear thesis: the next major productivity opportunity lies in the space between automated processes. Many factories have sophisticated machines and well-instrumented production lines, yet material still arrives through manual, disconnected workflows. The result is a familiar contradiction: a highly automated line can still depend on a forklift driver or an operator pushing a cart at its boundary.
“At the end of the line, there was a person driving a forklift and a person pushing a cart.”
That gap is where Rockwell is positioning production logistics. Rather than treating intralogistics as a stand-alone robotics project, the company describes an end-to-end workflow spanning production software, orchestration, controls, autonomous mobile robots, independent cart technology, and human work. This is a stronger industrial proposition than simply adding AMRs to a fleet. It treats the movement of work-in-process, components, packaging, and finished goods as part of the production system itself.
For manufacturers, the implication is significant. Material movement can become event-driven by production demand, quality status, inventory availability, and equipment conditions. The operational objective shifts from “dispatch a robot” to “maintain the production plan.”
From connected operations to autonomous response
Rockwell placed production logistics within a broader progression from connected operations to predictive and increasingly autonomous plants. Its “sense, think, act” framing is familiar in robotics, but the company extends the concept beyond the mobile robot to machines, lines, and plant-level workflows. Sensors establish context, software evaluates conditions, and physical assets execute the response, with a human retained in the loop where risk or uncertainty requires oversight.
“The right product to the right spot at the right time.”
This framing addresses one of the hardest problems in plant automation: local optimization does not automatically create system optimization. A packaging machine can be highly efficient while waiting for film. An assembly cell can meet its cycle time but starve because a component was not replenished in sequence. A warehouse can optimize picks while production priorities have already changed. The value of autonomy therefore depends on coordinating decisions across the workflow, not maximizing the utilization of each asset in isolation.
Rockwell’s stack: simulate, orchestrate, move
The press conference organized the production-logistics portfolio into three layers: simulation, orchestration, and movement. Together, these layers indicate how Rockwell intends to differentiate from robot-centric competitors and warehouse-only automation providers.
1. Simulate the operating model
Digital twins can validate layouts, traffic, throughput, safety zones, and control logic before equipment is commissioned. Rockwell also argued that major end users increasingly expect machine builders to provide a digital twin with the physical machine. In production logistics, that model has continuing value because routes, product mixes, cell configurations, and replenishment rules change over the asset lifecycle. A useful digital twin should therefore evolve from a commissioning tool into an operational decision-support asset.
2. Orchestrate work across people and assets
FactoryTalk Orchestration is central to the strategy. Rockwell said customer experience after its AMR acquisition revealed that the real challenge was coordinating robots with carts, people, machines, and software. That observation is directionally correct. Mixed environments will remain the norm for years, and manufacturers need workflow logic that can assign the next best task to an AMR, fixed system, or person while preserving production priorities.
The most compelling orchestration use case is dynamic response. If a supply-chain issue changes raw-material availability, the production schedule, material calls, and execution sequence should adjust together. This requires integration with manufacturing execution and production management systems, not merely fleet management.
3. Move material with the appropriate technology
Rockwell’s movement layer includes AMRs and independent cart technology, supplemented by robotics partners for applications such as palletizing. The portfolio reflects a practical reality: production logistics is not a single-robot category. Different workflows may require mobile transport, precise linear motion, storage and retrieval, or robotic handling. Competitive advantage will depend on coordinating these technologies as one workflow and integrating them to the control layer.
The Twinsburg case shows the value of integration
Rockwell used its Twinsburg, Ohio, plant as the principal proof point. The deployment began with autonomous material movement to reduce manual cart handling. The second phase integrated that capability with FactoryTalk production software, allowing the system to deliver the correct material in the required place, time, amount, and sequence.
According to the presentation, benefits from the first phase appeared in less than a month, while the interval between the first and second phases was approximately four to six months. Rockwell emphasized that workers were reassigned to higher-value plant roles rather than eliminated. The integrated phase reportedly reduced floor-space requirements and work-in-process, creating working-capital benefits in addition to labor-productivity gains.
“As soon as the pilot works, we immediately go to: how do we scale it across our facility?”
The case also illustrates an important adoption pattern. A transport-only pilot can establish safety, reliability, and workforce acceptance quickly. The larger business case emerges when the pilot is connected to production software and scaled across workflows. This is where manufacturers should measure schedule adherence, line starvation, work-in-process, floor-space consumption, indirect labor, and changeover performance, rather than focusing only on robot travel or labor displacement.
Manufacturing and warehousing are converging, but not becoming identical
Rockwell sees growing integration between production lines, adjacent warehouses, automated storage and retrieval systems, and shipping docks. Co-located manufacturing and warehousing make this convergence especially visible: components move from storage to assembly, finished goods move from the line to storage, and production priorities influence downstream handling.
However, Rockwell’s strongest position remains production logistics rather than general e-commerce fulfillment. The company can connect manufacturing software and controls to physical movement, whereas fulfillment specialists often optimize high-volume picking and seasonal labor flexibility. In warehouse environments, Rockwell must also integrate with warehouse management and warehouse execution systems. That makes interoperability, APIs, and ownership of workflow decisions crucial architectural questions.
Truck loading and unloading remain an important boundary. Rockwell described these applications as technically difficult because trailers vary, loads shift, and safety conditions are less controlled. This is a useful reminder that autonomous material flow will advance unevenly. Structured, repeatable movement inside the plant will automate faster than variable dock-edge work.
What manufacturers should do now
Start with a production constraint, not a robot count. Select a workflow where material availability affects throughput, such as line-side replenishment, packaging-material delivery, work-in-process transfer, or finished-goods evacuation. Define the baseline using line-starvation minutes, replenishment response time, indirect travel, and WIP.
Design the integration before the pilot. Document interfaces to MES or production management, ERP, WMS/WES, controls, safety systems, and identity services. A pilot that cannot exchange production status and task priorities may prove navigation but will not prove production value.
Model the mixed environment. Assume people, forklifts, carts, AMRs, conveyors, and fixed automation will coexist. Validate traffic, exceptions, manual recovery, charging, and safe-state behavior using a digital model before scaling.
Use phased economics. Separate phase-one transport savings from phase-two operational gains. The latter may include lower WIP, recovered floor space, better sequence adherence, fewer shortages, and higher OEE. These benefits often justify integration effort more than labor savings alone.
Build change management into commissioning. Create role-specific training for operators, maintenance, supervisors, controls engineers, and IT/OT teams. Define who owns workflow rules, exception handling, fleet availability, cybersecurity, and continuous improvement.
Analyst assessment
Rockwell’s production-logistics message is strategically credible because it aligns with the company’s installed base and its ability to integrate software, controls, motion, and robotics. The acquisition of an AMR platform supplied a visible physical asset, but orchestration is the more consequential layer. If Rockwell can make FactoryTalk Orchestration open enough to coordinate heterogeneous equipment and straightforward enough for plants to deploy repeatedly, it can compete for a broader share of the intralogistics architecture.
Execution risks remain. Manufacturers operate mixed fleets and multiple software systems, so closed or overly Rockwell-centric workflows would limit adoption. Digital-twin value also depends on maintaining models after commissioning, a discipline many plants have not established. Finally, the ROI claims in the transcript include several partially captured figures; buyers should request validated baselines, calculation methods, and comparable references before generalizing the Twinsburg results.
The larger trend is clear: production logistics is moving from an indirect support function toward a software-defined component of plant operations. The winners will not be determined only by the best mobile robot. They will be the suppliers that connect material movement to production intent, manage exceptions across people and machines, and turn successful pilots into repeatable plant-wide operating models.
The post Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy appeared first on Logistics Viewpoints.

Always-On AI Is Coming to Supply Chains. But Who Owns the Exception?

Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy
Beyond the AMR: Rockwell’s Production Logistics Strategy Connects Material Flow to Plant Autonomy
Freightos Global Freight Outlook – September 2026
Container rates jump another $1k/FEU – but is demand peaking? – July 8, 2026 Update

Walmart and the New Supply Chain Reality: AI, Automation, and Resilience
Trending
- Non classé3 mois ago
Freightos Global Freight Outlook – September 2026
- Non classé5 mois ago
Container rates jump another $1k/FEU – but is demand peaking? – July 8, 2026 Update
-
 Non classé2 ans ago
Walmart and the New Supply Chain Reality: AI, Automation, and Resilience
-
 Non classé7 mois ago
Why Sulfuric Acid Is Emerging as a Supply Chain Constraint in Copper
- Non classé6 mois ago
Container rates starting to spike on peak season rush – June 2, 2026 Update
- Non classé1 an ago
13 Books Logistics And Supply Chain Experts Need To Read
- Non classé1 an ago
Ex-Asia ocean rates climb on GRIs, despite slowing demand – October 22, 2025 Update
- Non classé5 mois ago
LCL Shipping Cost Calculator: Calculate Air and Sea Shipping Freight Rates